Roller wave and optical distortion: manufacturing effects versus restoration damage
Use repeatable reflections, viewing positions, fabrication records, and dry surface inspection to separate broad glass geometry from anisotropy, assembly deflection, contamination, and localized polishing lensing.
The reflection moves even when the glass is clean
Stand close to a facade and the building across the street may look straight. Walk back, and the same reflected roofline bends into a shallow wave. Move one bay sideways and the curve shifts again. Optical distortion is an interaction among glass shape, assembly pressure, reflected scene, viewing position, and light. It cannot be assigned to cleaning or polishing from one photograph.
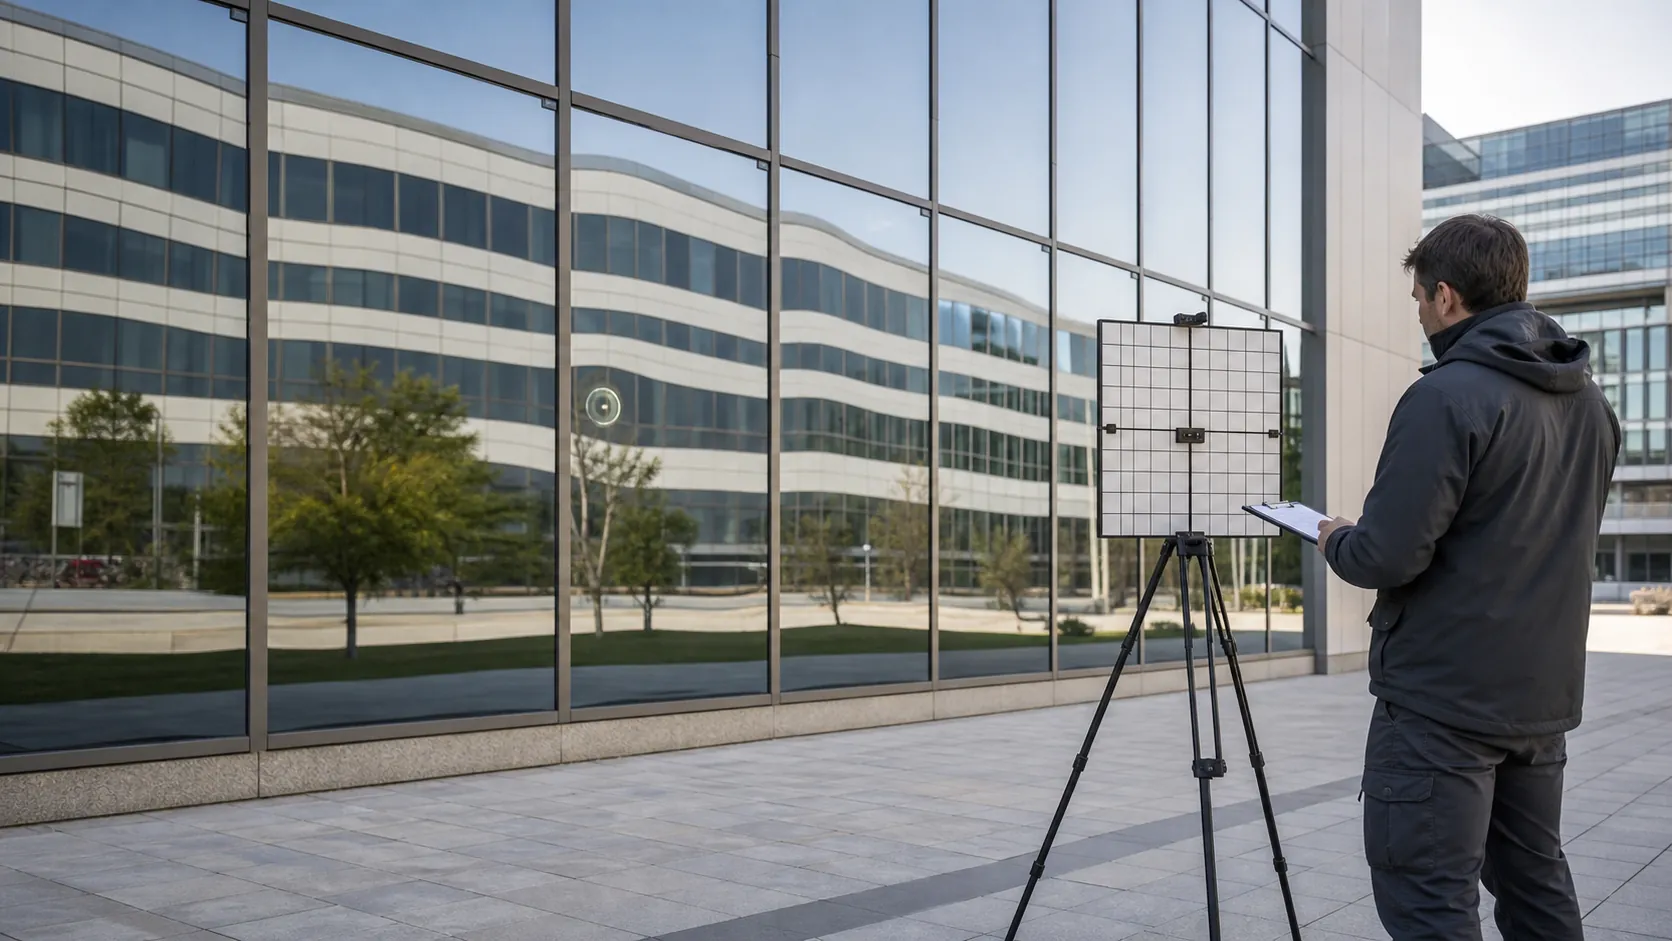
The useful question is not whether a reflection is perfectly straight. It is what physical condition produces the repeatable pattern and whether that condition changed during the work.
Know the geometric terms
| Condition | Typical geometry | Where it begins |
|---|---|---|
| Roller wave | Periodic peaks and valleys, commonly oriented with furnace travel | Glass softens and travels over rollers during heat treatment |
| Edge kink | Sharper change near a leading or trailing edge | Edge behavior during heating and cooling |
| Bow or warp | Broad curvature across much of the lite | Fabrication, lamination, heat treatment, or assembly condition |
| IGU deflection | Large smooth inward or outward curvature that can vary with environment | Pressure and temperature differences, altitude, glass size, and construction |
| Glazing or structural deflection | Shape changes with frame pressure, wind, support, or load | Installed system rather than only the glass sheet |
| Polishing lensing | Localized magnification, compression, swirl, or ripple around a worked area | Uneven material removal or transition during restoration |
Vitro notes that heat treatment modifies the original flatness of annealed glass and can produce roller wave, bow, and warp. Other causes include laminates, thin constructions, glazing pressure, wind, temperature, barometric pressure, and fabrication-to-installation altitude change.
Do not confuse shape with anisotropy
Anisotropy is a polarized-light effect related to residual stress, not a simple map of surface height. It may appear as dark bands, circles, or colors under blue sky or polarized sunglasses. Roller wave bends reflected straight lines because the glass geometry varies.
A pane can show both. It can also show coating color variation, insulating-glass interference fringes, suction-cup residue, mineral deposit, scratches, or polish haze. Classify each observation instead of forcing them into one cause.
Build a repeatable viewing station
- Identify the elevation and lite on drawings. Record glass type, thickness, heat treatment, coating, laminate, and insulating-unit construction.
- Clean only enough to remove confirmed loose surface material, then let the glass dry.
- Select a reflected scene with straight high-contrast lines, such as mullions or a roof edge. Avoid tree branches as the only reference.
- Mark distance, height, horizontal position, and camera focal length. Keep the lens level and disable automatic perspective correction when possible.
- Capture the full lite and neighboring lites before making close views.
- Move along a measured path and note whether the bend repeats across the pane, follows the furnace direction, changes broadly, or stays centered on a worked patch.
- Repeat under comparable wind and temperature if assembly deflection is suspected.
A grid held against the glass is not the same as a reflected grid at a distance. The first can help inspect local surface artifacts; the second reveals optical power across the viewing path. State which method was used.
Look for the signature of restoration work
Glass polishing removes a shallow amount of material. If removal is too deep, uneven, or poorly blended, the worked area can act as a weak lens. Reflections may enlarge on one side, compress on another, or form a localized ring. Fine directional scratches, haze, or a rotating-tool pattern may appear in raking light.
Compare the suspected area with work maps, test-panel boundaries, abrasive sequence, tool size, pass direction, dwell, temperature log, and final inspection photographs. A distortion that continues with similar spacing across untouched lites is less consistent with a small polishing pad. A defect that begins and ends precisely at the restoration boundary deserves focused assessment.
Do not repolish merely because the area looks different while wet. Water changes reflection and fills texture. Dry it, inspect from agreed positions, and confirm whether the issue is residual scratch, haze, abrupt transition, or optical power.
Use measurements for the question they can answer
Peak-to-valley roller-wave gauges, scanners, and optical systems can quantify flatness or optical power when used by qualified parties. Project specifications may use physical flatness, millidiopters, a mockup, or appearance criteria. These measures are not interchangeable.
Vitro states that there is no single industry standard that quantifies permissible heat-treated roller wave for every project and recommends full-scale mockups under job-site conditions to reduce surprises. A commonly specified number does not guarantee acceptable appearance in a particular reflected scene.
Before dispute testing, agree on instrument, calibration, grid, edge exclusion, orientation, sample size, environmental conditions, and acceptance rule. Otherwise two accurate measurements may answer different questions.
Separate responsibility with a before-and-after record
Before restoration, photograph each test pane dry from the future acceptance positions. Include full-lite reflections and close surface views in broad and raking light. Record roller-wave direction, existing bow, anisotropy, coating variation, IGU deflection, scratches, and frame pressure clues.
After each abrasive stage, check the transition around the work, not only the deepest defect. Final documentation should repeat the same positions, camera setup, time window when practical, and dry condition. This makes a genuine change visible without blaming the contractor for geometry that was present in the fabricated lite.
What cleaning and polishing cannot do
Cleaning removes compatible surface contamination. It does not flatten heat-treated glass, relieve residual stress, change an insulating-unit pressure difference, or correct frame load. Polishing may remove selected scratches or surface alteration, but it cannot erase broad roller wave. Trying to grind the entire lite flat would change thickness, optics, coatings, strength assumptions, and product status.
If the issue is localized restoration lensing, a specialist can assess whether a larger controlled blend is feasible. That decision depends on remaining glass thickness, defect depth, coating, heat treatment, location, safety role, access, and the optical acceptance standard. Replacement may be the responsible option when correction would require excessive removal or still leave objectionable optics.